2026-09-19
Share This Article
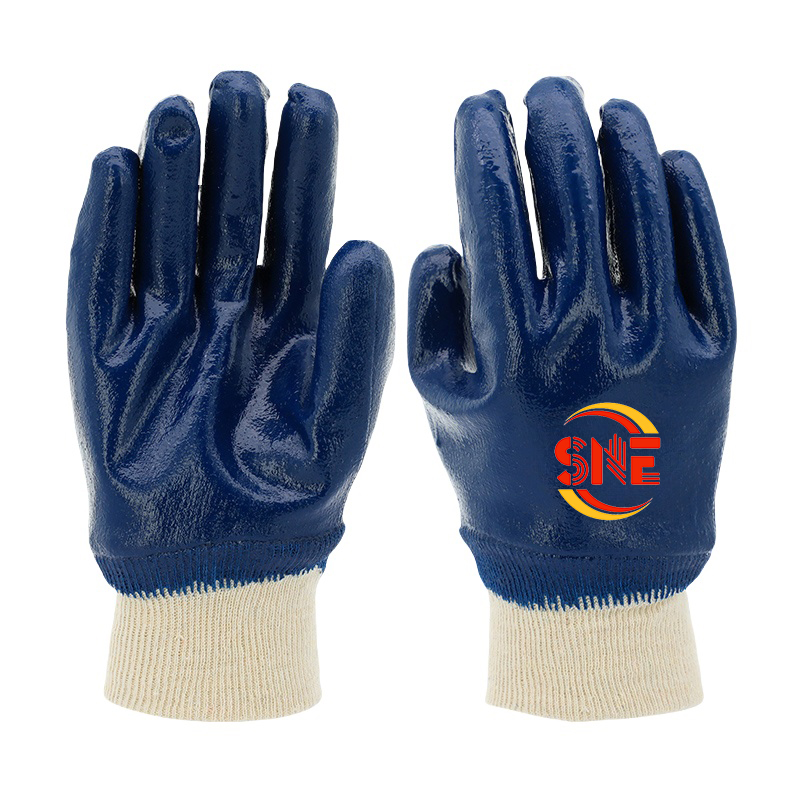
Waterproof Oil Resistant Gloves Suppliers in the United States
Quick Answer

If you need waterproof oil resistant gloves for demanding job sites in the United States, the most practical short list includes Ansell, Honeywell, MCR Safety, Superior Glove, Showa, and Ergodyne because these brands are widely specified across construction, oil and gas, utilities, warehousing, sanitation, and heavy maintenance. For buyers who need fast replenishment, nationwide distributor coverage, and dependable compliance documentation, these suppliers are the safest starting point for field trials and bulk purchasing.
For local sourcing, buyers in Houston, Chicago, Los Angeles, Atlanta, and New Jersey usually prioritize gloves with strong grip in oily conditions, waterproof barriers for outdoor or washdown work, and lining options suited to heat or cold. Ansell is often selected for chemical and industrial applications, Showa for liquid-proof hand protection and grip performance, MCR Safety for broad industrial availability, Honeywell for integrated PPE purchasing, Superior Glove for task-specific hand protection, and Ergodyne for construction and utility crews needing durable performance gear.
Qualified international suppliers can also be a smart option. Buyers in the United States frequently consider certified overseas manufacturers, including Chinese factory-direct producers, when they need OEM branding, stable bulk capacity, and better cost-performance. This is especially relevant for importers, wholesalers, and private-label buyers who want waterproof oil resistant gloves with local-compliance documentation, responsive pre-sales guidance, and dependable after-sales support.
United States Market Overview

The market for waterproof oil resistant gloves in the United States is driven by a mix of safety regulation, labor shortage pressures, higher replacement rates in harsh environments, and the push for better productivity on job sites. In practical terms, employers are no longer buying gloves as a commodity alone. They are evaluating injury prevention, grip performance, durability per shift, and how glove design affects worker acceptance. That matters in sectors such as oil and gas in Texas, port logistics in Los Angeles and Long Beach, food processing in the Midwest, public works in the Northeast, and marine maintenance around the Gulf Coast.
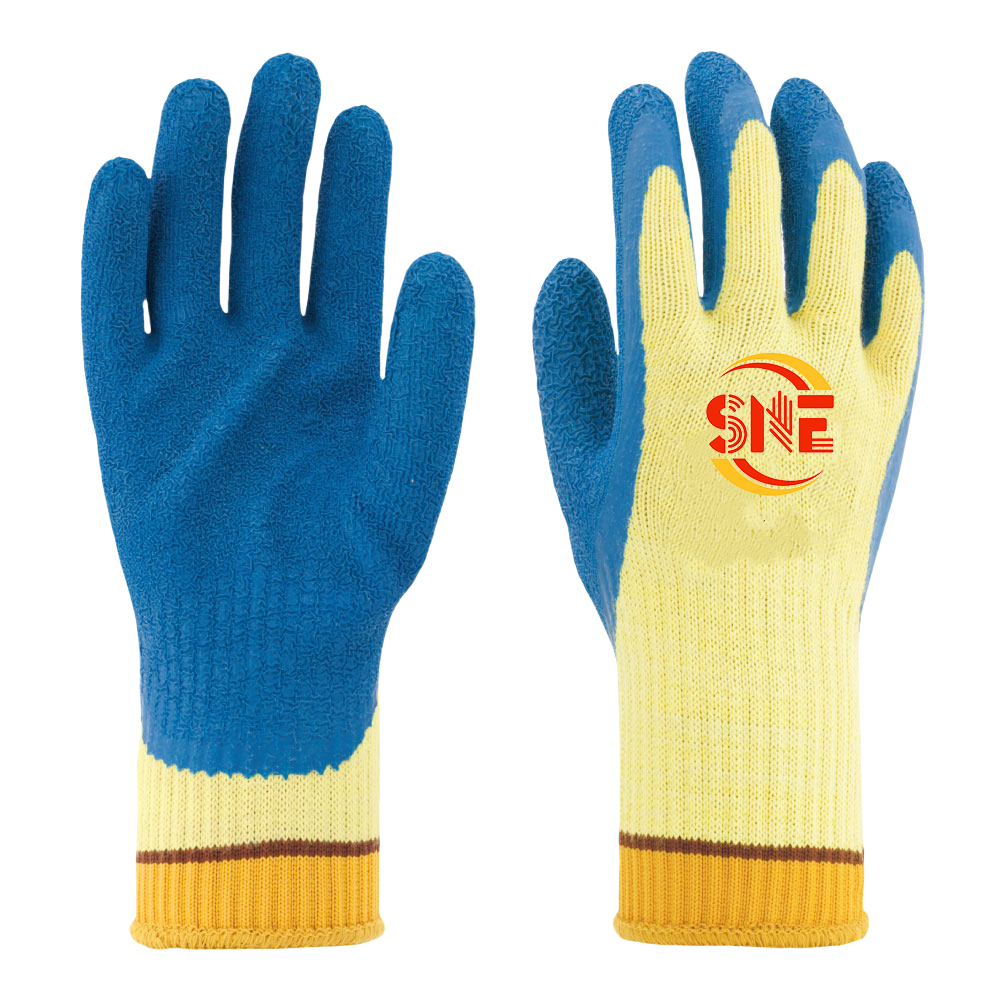
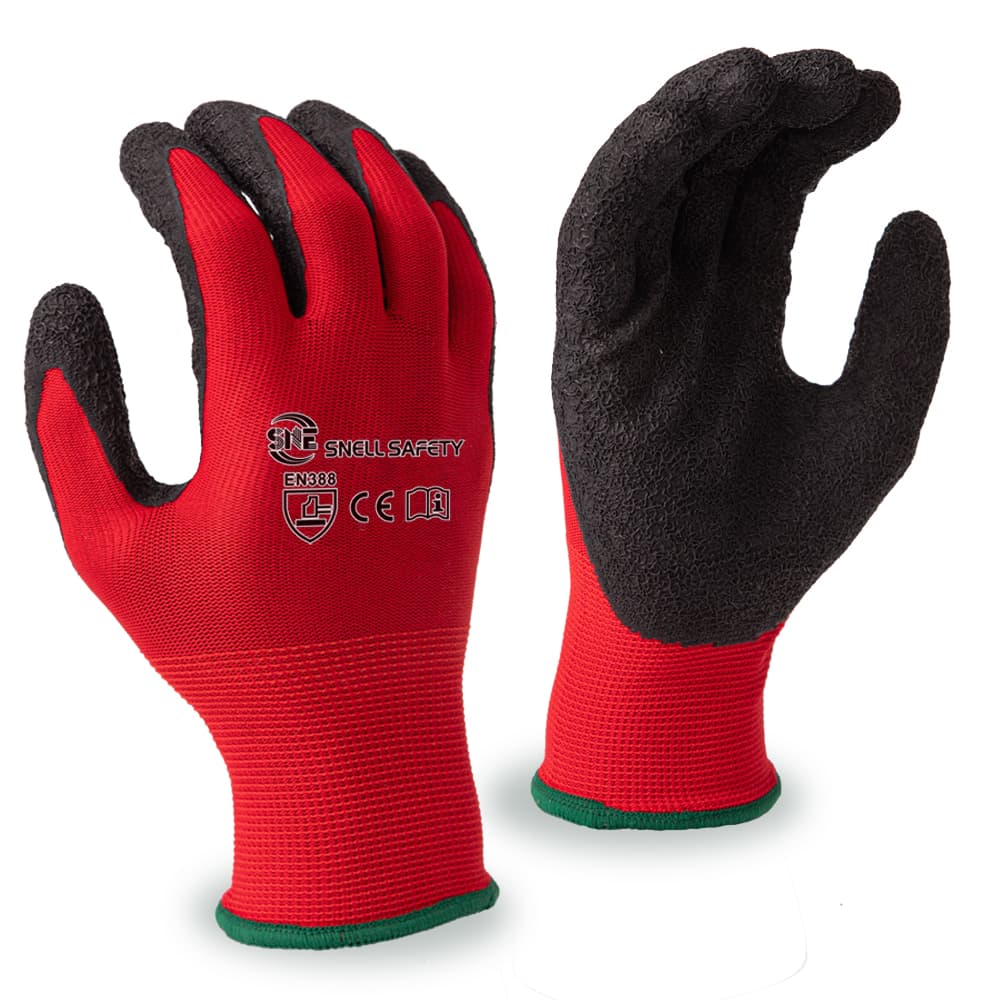
Demand is especially strong where workers face water, lubricants, fuels, grease, coolants, mud, detergents, and fluctuating temperatures in the same shift. Traditional knit gloves or light disposable gloves are not enough in these settings. Buyers increasingly want layered performance: waterproof protection, oil grip, abrasion resistance, and in many cases cut resistance or impact protection. This creates a large market segment for fully coated nitrile gloves, PVC-supported gloves, double-dipped gloves, insulated liquid-proof gloves, and specialty chemical-resistant styles.
The United States also has a unique distribution pattern. Large national distributors supply enterprise customers with managed inventory programs, while regional safety houses serve municipal crews, contractors, warehouses, and local manufacturers. Around major logistics corridors such as Dallas-Fort Worth, Savannah, Memphis, and the Inland Empire, glove consumption is high because of turnover-heavy operations and broad seasonal demand. Coastal and energy markets create further specialization, especially for gloves that must maintain dexterity under wet and oily conditions.
The line chart above illustrates a realistic demand-growth pattern for the U.S. market. The rise reflects expansion in energy maintenance, infrastructure upgrades, stricter PPE procurement, and the replacement of low-performance commodity gloves with more specialized waterproof and oil-grip products. Buyers should read this trend as a signal that lead-time planning and supplier diversification are becoming more important, especially before winter maintenance cycles and hurricane-related recovery seasons.
Top Suppliers in the United States

| Company | Headquarters / Service Region | Core Strengths | Key Offerings | Best Fit Buyers |
|---|---|---|---|---|
| Ansell | Serves all major U.S. industrial regions through national distribution | Strong industrial and chemical protection portfolio, global compliance support, broad specification acceptance | Liquid-resistant nitrile gloves, chemical-resistant gloves, cut-resistant coated gloves | Large manufacturers, chemical plants, utilities, national contractors |
| Honeywell | Nationwide U.S. coverage with strong enterprise and institutional reach | Integrated PPE sourcing, broad industrial catalog, support for large procurement programs | Coated work gloves, liquid-resistant gloves, task-specific industrial hand protection | Enterprise procurement teams, municipalities, transportation fleets |
| MCR Safety | Strong distributor presence across the South, Midwest, and nationwide | Industrial breadth, reliable stocking options, durable glove designs for dirty environments | PVC gloves, nitrile-coated gloves, supported liquid-proof gloves | Construction firms, warehouses, fabrication shops, maintenance teams |
| Superior Glove | Wide U.S. service through industrial distributors and safety partners | Task-specific engineering, advanced grip and cut-resistance combinations, premium application fit | Water-resistant and oil-grip gloves, cold-weather gloves, cut-resistant coated models | Metalworking, automotive, heavy industry, safety-led employers |
| Showa | Well-established U.S. industrial distribution network | Liquid-proof glove expertise, ergonomic fit, strong coatings and finish quality | Fully coated nitrile gloves, chemical-resistant gloves, insulated waterproof styles | Oil and gas, janitorial, agriculture, food-adjacent industrial users |
| Ergodyne | Broad U.S. job-site and contractor distribution coverage | Job-site practicality, worker comfort focus, strong visibility in construction and utilities | Worksite gloves, cold-weather waterproof gloves, high-grip utility styles | Contractors, utilities, telecom crews, municipal field teams |
| Youngstown Glove | Strong U.S. presence in utility and field-service channels | Performance features for field work, durable constructions, user-focused fit | Water-resistant work gloves, reinforced palm gloves, winter utility gloves | Utilities, line crews, field service technicians |
This table gives a practical starting point rather than a theoretical ranking. Each supplier has a different advantage. Ansell and Honeywell are often preferred in large formal procurement systems. Showa is strong when buyers need dependable liquid protection and grip. MCR Safety is widely used where availability and value matter. Superior Glove stands out in applications that combine multiple hazards. Ergodyne and Youngstown Glove are often chosen by crews that value fit, comfort, and field durability.
Product Types That Match U.S. Job-Site Needs
Not all waterproof oil resistant gloves perform the same way. In the United States, selection usually depends on whether the hazard is brief contact with oils, immersion in liquids, repetitive handling of slick materials, outdoor winter exposure, or a combination of abrasion and contamination. A glove that works well in a refinery turnaround may not be ideal for stormwater maintenance or refrigerated logistics.
| Product Type | Construction | Primary Benefit | Common U.S. Uses | Limitation to Watch |
|---|---|---|---|---|
| Fully coated nitrile gloves | Seamless liner with full nitrile coating | Excellent oil resistance and solid abrasion performance | Automotive, equipment repair, warehouse maintenance | Can run warm in hot climates |
| Double-dipped nitrile gloves | Base coating plus textured second nitrile layer | Better grip in wet and oily handling | Construction, drilling support, steel handling | May reduce fine dexterity |
| PVC supported gloves | Cotton or jersey liner with PVC outer shell | Good waterproof barrier and economical bulk value | Sanitation, fisheries, general maintenance, washdown | Less breathable, moderate dexterity |
| Sandy nitrile palm-coated gloves | Palm coating with textured finish | Grip on oily parts with better hand feel | Assembly, shipping, mechanical work | Not fully waterproof |
| Insulated waterproof gloves | Waterproof shell with thermal lining | Cold protection plus liquid resistance | Utilities, winter construction, snow operations | Bulkier profile |
| Chemical-resistant gauntlet gloves | Long cuff supported or unsupported design | Extended splash protection and forearm coverage | Cleaning chemicals, degreasers, industrial processing | May be excessive for light tasks |
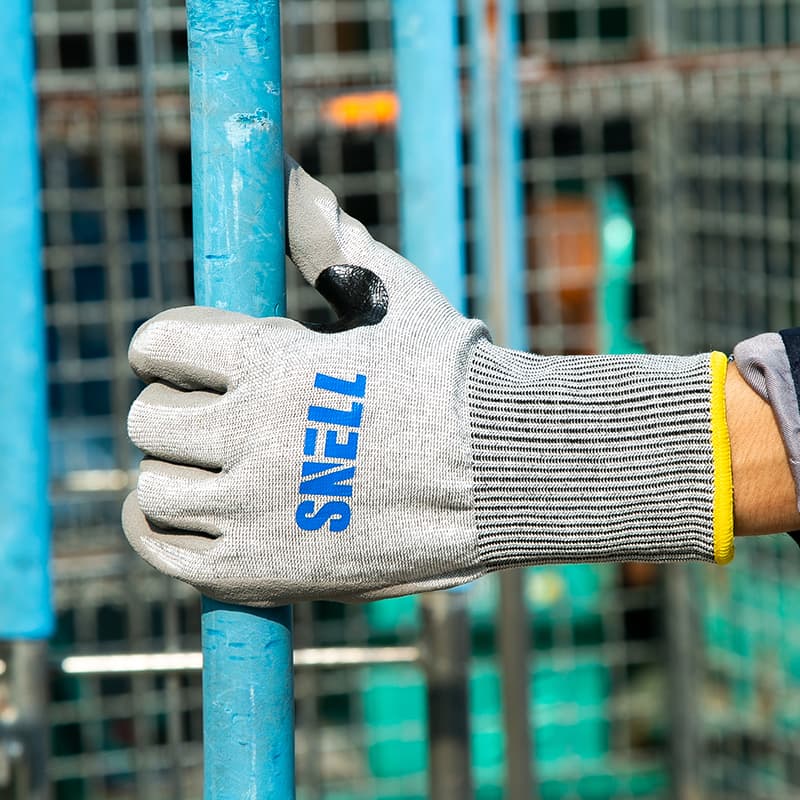
| Cut-resistant waterproof gloves | Engineered liner with full or partial coating | Multi-hazard protection in wet environments | Glass, metal fabrication, recycling, heavy maintenance | Higher unit price |
The best choice comes down to balancing barrier performance, grip, dexterity, thermal comfort, and lifecycle cost. A glove that costs more per pair can still reduce total spend if it lasts longer, reduces slips, and prevents rejected inventory or injuries. Buyers in the United States increasingly ask suppliers for wear-trial support instead of selecting solely by catalog description.
Industry Demand Across the United States
Different industries purchase waterproof oil resistant gloves for different reasons. Oil and gas teams may emphasize hydrocarbon contact and grip on tools. Food-adjacent industrial users may care more about washdown conditions and sanitation changeovers. Construction firms want gloves that survive mud, rain, concrete residue, and equipment lubrication. Utilities often require all-weather performance with enough feel for routine tasks.
This bar chart shows how demand is distributed across key end-use sectors in the United States. Oil and gas, construction, and manufacturing remain major drivers because they combine heavy wear with contamination risk. Utilities and warehousing follow because weather and handling efficiency matter. Marine and sanitation are more specialized but still important in coastal states and municipal procurement.
Buying Advice for U.S. Procurement Teams
When selecting waterproof oil resistant gloves, buyers should avoid a single-question purchase process. The better method is to define exposure type, grip surface, work duration, climate, and whether workers handle sharp edges or vibrating tools. This reduces the chance of buying gloves that look strong on paper but fail in real use.
Start with coating selection. Nitrile is usually the best all-round choice for oily industrial handling because it combines oil resistance, abrasion durability, and broad user acceptance. PVC is often attractive for lower-cost liquid protection and sanitation tasks. Latex can provide good flexibility and wet grip in some settings, but it may not be ideal when oil contact is the main issue. If workers face both cutting and liquids, look at engineered liners with full coatings rather than treating cut protection as a separate purchase.
Next, review cuff length and coverage. In many U.S. applications, wrist-length gloves are enough for tool handling, assembly, and general maintenance. But for washdown, tanker handling, drain cleaning, or chemical splash, gauntlet or extended-cuff styles are more appropriate. For outdoor winter crews in states such as Minnesota, Michigan, New York, and Colorado, thermal lining can improve compliance because workers are less likely to remove gloves during tasks.
Bulk buyers should also ask suppliers for documentation on coating consistency, liner gauge, test methods, carton configuration, and replenishment lead times. Distributor stock can solve urgent needs, but long-term contracts often benefit from direct factory programs or dual sourcing. Buyers importing through ports such as Los Angeles, Savannah, Houston, or New York/New Jersey often blend domestic inventory with overseas factory supply to reduce cost without sacrificing continuity.
| Buying Criterion | Why It Matters | Questions to Ask | Best For | Risk If Ignored |
|---|---|---|---|---|
| Oil grip texture | Reduces slips and dropped parts | Is the finish sandy, foam, smooth, or double-dipped? | Mechanical and material handling work | Productivity loss and hand fatigue |
| Waterproof coverage | Determines barrier level | Is the glove fully coated or palm coated only? | Outdoor and washdown tasks | Wet hands and lower worker acceptance |
| Abrasion resistance | Affects life per pair | What wear performance data is available? | Construction and heavy maintenance | Frequent replacement and higher total cost |
| Temperature suitability | Comfort drives compliance | Is there insulated or breathable construction? | Cold storage and winter field work | Workers remove gloves during tasks |
| Cut protection | Needed in mixed-hazard work | Does the glove combine cut resistance with liquid protection? | Metal, glass, recycling, fabrication | Under-protection or duplicate PPE spending |
| Supply reliability | Supports uninterrupted operations | What are stock levels, lead times, and backup plans? | National and multi-site buyers | Shortages during peak demand |
| Customization options | Helps private label and program fit | Can the supplier support OEM, sizing, branding, packaging? | Distributors and brand owners | Limited market differentiation |
The explanation behind this checklist is straightforward: a glove purchase should be treated as an operational decision, not only a price decision. Grip, comfort, and continuity often affect real cost more than unit price alone. The most effective procurement teams in the United States validate gloves through field trials, then negotiate long-term supply based on measured wear life and user feedback.
Applications by Sector
Construction crews use waterproof oil resistant gloves for trenching, utility installation, concrete forming, site cleanup, and machinery handling. In these jobs, mud and rain combine with fuel residue, grease, and abrasive materials. A palm-coated glove may work for lighter handling, but full coating is often better when workers kneel, lift wet materials, or face repeated contact with slurry and dirty water.
Oil and gas operations across Texas, Louisiana, Oklahoma, and North Dakota frequently require gloves that hold grip when exposed to drilling fluids, oils, and slick metal surfaces. In pipeline maintenance and tank farm operations, a poor grip glove can increase dropped-tool incidents and slow task completion. Workers also value a fit that allows secure tool control while maintaining a liquid barrier.
Manufacturing and metalworking facilities in states such as Ohio, Indiana, Pennsylvania, and Illinois often need gloves that combine oil resistance with cut protection. Machine oils and coolants make surfaces slippery, while stamped parts and metal edges introduce laceration hazards. In these settings, advanced coated cut-resistant gloves often deliver better protection and better worker acceptance than separate glove layers.
Warehousing and logistics centers around Chicago, Dallas, Atlanta, and Southern California use these gloves in equipment maintenance, returns processing, yard work, and refrigerated or wet handling tasks. While the hazard level may be lower than in heavy industry, glove comfort matters more because workers perform repetitive movements over long shifts. A glove that is too stiff or too hot can reduce throughput.
Public works departments and utilities require all-weather gloves for water main maintenance, roadside repairs, storm cleanup, and fleet servicing. Municipal buyers often need standardization across multiple departments, which is why gloves with balanced performance and broad sizing ranges tend to win bids. Ease of training and predictable replacement cycles are also important.
Trend Shift in Product Preference
This area chart highlights a major market change: United States buyers are gradually moving from basic commodity gloves to more advanced multi-hazard options. That shift reflects a stronger focus on injury prevention, worker retention, and measurable productivity. It also explains why suppliers offering testing support, sizing consistency, and task-specific designs are gaining traction with industrial buyers.
Case Studies from Realistic U.S. Purchasing Scenarios
A Texas equipment maintenance contractor replaced a low-cost PVC glove with a textured full-nitrile style after repeated complaints about poor grip on oily hydraulic parts. The new glove had a higher unit cost, but wear life improved and the contractor reduced mid-shift glove changes. Supervisors also reported fewer dropped fasteners during wet-weather service calls. The lesson was simple: better grip and comfort lowered actual operating cost.
A Midwest food-adjacent packaging plant needed a waterproof glove for washdown crews and maintenance technicians. One group needed strong liquid protection, while the other needed dexterity and occasional cut resistance. Instead of standardizing on one glove, the buyer split the program into supported gauntlet gloves for sanitation and cut-resistant coated gloves for maintenance. This reduced over-specification and improved worker satisfaction.
A Gulf Coast port service provider faced seasonal spikes in glove demand during storm recovery and marine equipment repair. Domestic stock was reliable but expensive during surge periods. The company adopted a mixed sourcing model: domestic distributor stock for emergencies and imported private-label gloves for planned replenishment. By tying forecasts to vessel traffic and weather seasons, the buyer stabilized supply and reduced average spend.
Local Suppliers and Distribution Realities
In the United States, many glove purchases happen through distributors rather than direct manufacturer accounts, especially for small and mid-sized companies. That does not make direct factory sourcing less relevant. It simply means the buying model should match order size, urgency, and the need for customization. A local contractor may prefer nearby stock through a safety distributor in Houston or Phoenix, while a private-label wholesaler may import container quantities through Long Beach or Savannah.
| Supplier Channel | Typical Region | Main Advantage | Common Buyer Type | When to Use It |
|---|---|---|---|---|
| National industrial distributor | All 50 states | Fast replenishment and integrated purchasing | Large multi-site employers | Standardized national glove programs |
| Regional safety house | Texas, Midwest, Northeast, Southeast, West Coast | Closer service and local inventory | Contractors and local manufacturers | Frequent smaller-volume orders |
| Direct manufacturer account | Major metro and industrial hubs | Technical support and program pricing | Enterprise buyers | Large annual volume commitments |
| Factory-direct importer | Ports and inland logistics hubs | Lower landed cost and OEM flexibility | Wholesalers, brand owners, distributors | Private label and bulk procurement |
| Online industrial platform | Nationwide | Easy comparison and quick ordering | Small business buyers | Spot buys and urgent reorders |
| Municipal bid supplier | State and local government markets | Contract familiarity and documentation support | Public works and utilities | Bid-driven procurement cycles |
The explanation here is that the best supplier is often not just a brand but a delivery model. U.S. buyers should select the channel that matches their inventory risk, customization needs, and support expectations. Fast local delivery matters for emergency maintenance. Factory-direct sourcing matters more for consistent long-run savings and private-label growth.
Supplier Comparison for Buyers
This comparison chart is not a universal ranking. It shows how buyers often evaluate overall value by blending availability, application fit, technical support, customization, and cost. Domestic brands score well on immediate access and known documentation. Factory-direct import models score strongly where buyers prioritize OEM programs, container economics, and product customization.
Our Company
For United States buyers exploring a factory-direct alternative, Snell Safety presents a practical option because its industrial glove production is built around recognized coating technologies including PU, latex, and nitrile, supported by ISO 9001 and CE-certified quality systems that help document consistent manufacturing and testing discipline for international markets. With two manufacturing facilities, 6 production lines, more than 150 trained employees, and daily output capacity of 150,000 pairs, the company has the scale to support importers, distributors, dealers, brand owners, industrial end users, and even smaller private-label projects through flexible OEM, ODM, wholesale, custom packaging, sizing, and branding programs. For the United States market, that matters because buyers often need both stable bulk capacity and the ability to tailor gloves for regional applications such as Gulf Coast oil service, Midwest manufacturing, or West Coast logistics. Through its export experience across North America-linked trade flows and multilingual commercial support, the company operates with the responsiveness expected by U.S. buyers, combining online consultation, sample development, specification matching, and after-sales follow-up with long-term account support rather than acting like a remote transactional exporter; buyers can explore its product range at industrial glove catalog, review company background via Snell Safety, or start a specification discussion through its U.S. buyer contact channel.
How to Evaluate a Factory-Direct International Supplier
International sourcing makes the most sense when a U.S. buyer needs custom branding, better pricing on volume, dedicated production slots, or glove specifications that local stock programs do not fully support. But factory-direct should not mean compromising on control. Buyers should request samples, technical data, packaging details, inspection methods, and landed-cost scenarios before committing.
Ask whether the supplier can support multiple coatings, liner gauges, cuff styles, and logo methods. Review lead times from production to port departure, then compare them with your inventory cycles. For imports into the United States, buyers often model entry through Los Angeles, Oakland, Houston, Savannah, or New York/New Jersey depending on final delivery points. Inland distribution costs can materially affect the true savings of an imported glove program.
Pre-sales and after-sales support also matter. A serious supplier should be able to discuss application matching, trial quantities, replacement recommendations, and corrective action if a batch issue arises. For distributors and brand owners, packaging consistency and barcode support are just as important as coating performance. Buyers should treat these operational details as part of product quality.
Future Trends Through 2026
Looking ahead to 2026, several trends are shaping the U.S. market for waterproof oil resistant gloves. The first is smarter material engineering. More buyers are looking for gloves that combine liquid protection with cut resistance, touchscreen usability, lower hand fatigue, and improved breathability. This trend is especially visible in logistics, field service, and advanced manufacturing where workers want one glove to handle multiple job conditions.
The second trend is policy and documentation pressure. Safety managers increasingly need products that fit internal PPE matrices, insurance expectations, and more formal supplier-approval processes. That means traceability, test records, and consistent SKU performance will matter more. Suppliers who can back claims with structured quality systems and repeatable production standards will hold an advantage.
The third trend is sustainability. U.S. buyers are asking more questions about packaging reduction, production efficiency, longer glove lifespan, and how to cut waste from high-turnover PPE categories. Even when sustainability is not the main purchase driver, durability and reduced replacement frequency align with both environmental and economic goals. Over time, procurement teams are likely to favor gloves that last longer and support better inventory planning.
A fourth trend is channel hybridization. More companies will keep emergency stock domestically while developing direct-import programs for planned demand. This mixed model helps protect against port disruption, storm seasons, and sudden industrial demand spikes. It also gives procurement teams more leverage when balancing cost and service.
FAQ
What is the best material for waterproof oil resistant gloves?
For most industrial applications in the United States, nitrile is the top all-round choice because it handles oils well, provides good abrasion resistance, and supports strong grip finishes. PVC remains useful for fully waterproof, value-oriented applications such as sanitation and general maintenance.
Are all oil resistant gloves fully waterproof?
No. Many gloves are only palm coated, which improves grip on oily surfaces but does not keep the entire hand dry. If workers face standing water, washdown, or rain exposure, look for fully coated or fully supported waterproof styles.
Which industries buy the most waterproof oil resistant gloves in the United States?
Oil and gas, construction, manufacturing, utilities, warehousing, marine services, and sanitation are among the largest demand segments. The exact product specification varies by task, climate, and exposure type.
Should U.S. buyers source domestically or import directly?
Both can work well. Domestic sourcing is ideal for immediate replenishment, short lead times, and local stock needs. Direct import is often better for OEM projects, private label, and large-volume cost optimization. Many buyers use both strategies together.
What should I ask for before approving a bulk glove order?
Request samples, technical specifications, size details, coating information, packaging format, inspection standards, lead times, and any available compliance documentation. Field trials with actual workers are highly recommended before final rollout.
How often should gloves be replaced?
Replacement depends on abrasion, contamination, and loss of grip or barrier integrity. High-performing waterproof oil resistant gloves may cost more upfront but often lower total replacement frequency and improve worker acceptance.
Do I need insulated gloves for outdoor work?
In colder states or winter seasons, yes. Workers handling wet materials outdoors often need insulated waterproof gloves to maintain dexterity and compliance. Otherwise, they may remove gloves to warm hands or improve movement.
Conclusion
For buyers in the United States, the best waterproof oil resistant gloves are those that match real job-site exposure rather than generic catalog claims. Local buyers should compare trusted brands such as Ansell, Honeywell, MCR Safety, Superior Glove, Showa, and Ergodyne, while also considering factory-direct international partners when customization, pricing, and long-run supply security matter. The strongest procurement results usually come from field testing, channel diversification, and selecting gloves by total operating value instead of unit price alone.